

Cleaning 240 product variants
Cleaning a variety of products and batch sizes
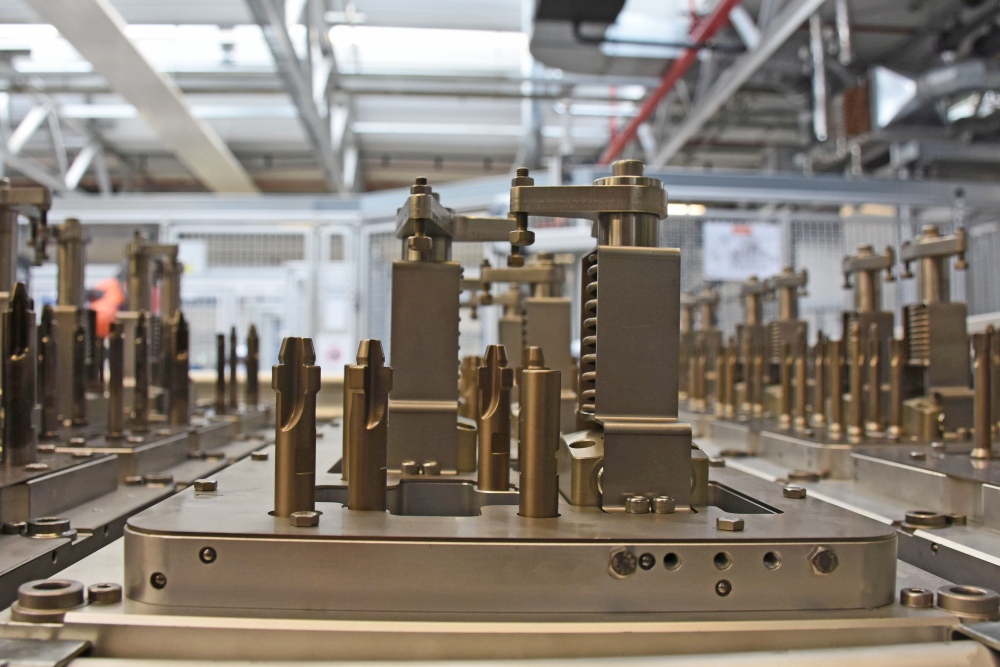
A manufacturer of drive and control technology integrates a cleaning system into its production line, which cleans around ten different component families automatically and in the production cycle. The targeted individual part cleaning of the approximately 240 very different workpieces is achieved with the help of a sophisticated feed system.
As part of a restructuring of production, a new interlinked production line was created in the Industrial Hydraulics division at Bosch Rexroth AG. With its products, the internationally active supplier of drive and control technology ensures efficient, powerful and safe movement in machines and systems of all types and sizes. Based in Lohr, Bavaria, the company combines practical experience and know-how in the market segments of mobile applications, plant engineering and construction, and factory automation. The range of products for this includes mobile and industrial hydraulics, electric drive and control technology, gear technology, and linear and assembly technology, including software and interfaces for fully networkable applications.
Following a restructuring of production, the industrial hydraulics division based at the company's headquarters concentrates on technically sophisticated, complex products manufactured in batch sizes of one to around 5,000 units. The low quantities compared to classic series production with batch sizes of 100,000 parts or more required an adjustment of the production capacities. "We have therefore set up an interlinked production line with seven processing machines. It enables the fully automated precision machining of components from ten component families with around 240 material numbers and unit weights of one to twelve kilograms," specifies Erik Müller, who as overall project manager is responsible for the implementation of the new production line at Bosch Rexroth.
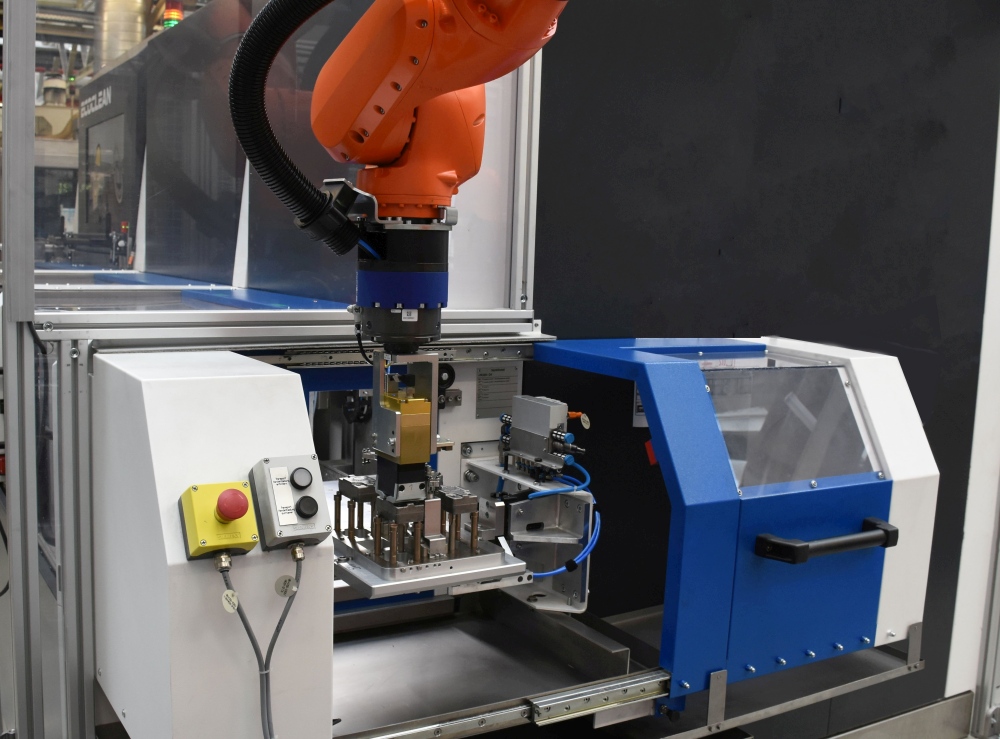
Interlinked production line
Within this production system, process-specific workpiece carriers form the interface to the respective machine. Workpiece handling, i.e. clamping and unclamping of the parts, is performed by robots. To remove residues from previous machining processes, a cleaning system is integrated into the finishing line.
"In the past, the workpieces of different component families were cleaned in separate systems. By merging them, it was important that the new cleaning system could be used for the very large variety of workpieces and the different batch sizes, as well as enabling simple and fast creation of part-specific cleaning programs. In addition, the specified product-specific particulate cleanliness specifications and a surface tension of greater than 38 millinewtons/meter must be achieved within the specified cycle times of 16 to 55 seconds," says Eva Nowak, project manager for cleaning technology at Bosch Rexroth, describing some of the requirements for selecting the new cleaning system.
The project team decided on the EcoCvelox from Ecoclean, which was still under development at the time. This was preceded by discussions with several manufacturers of cleaning systems.

Wide range of components
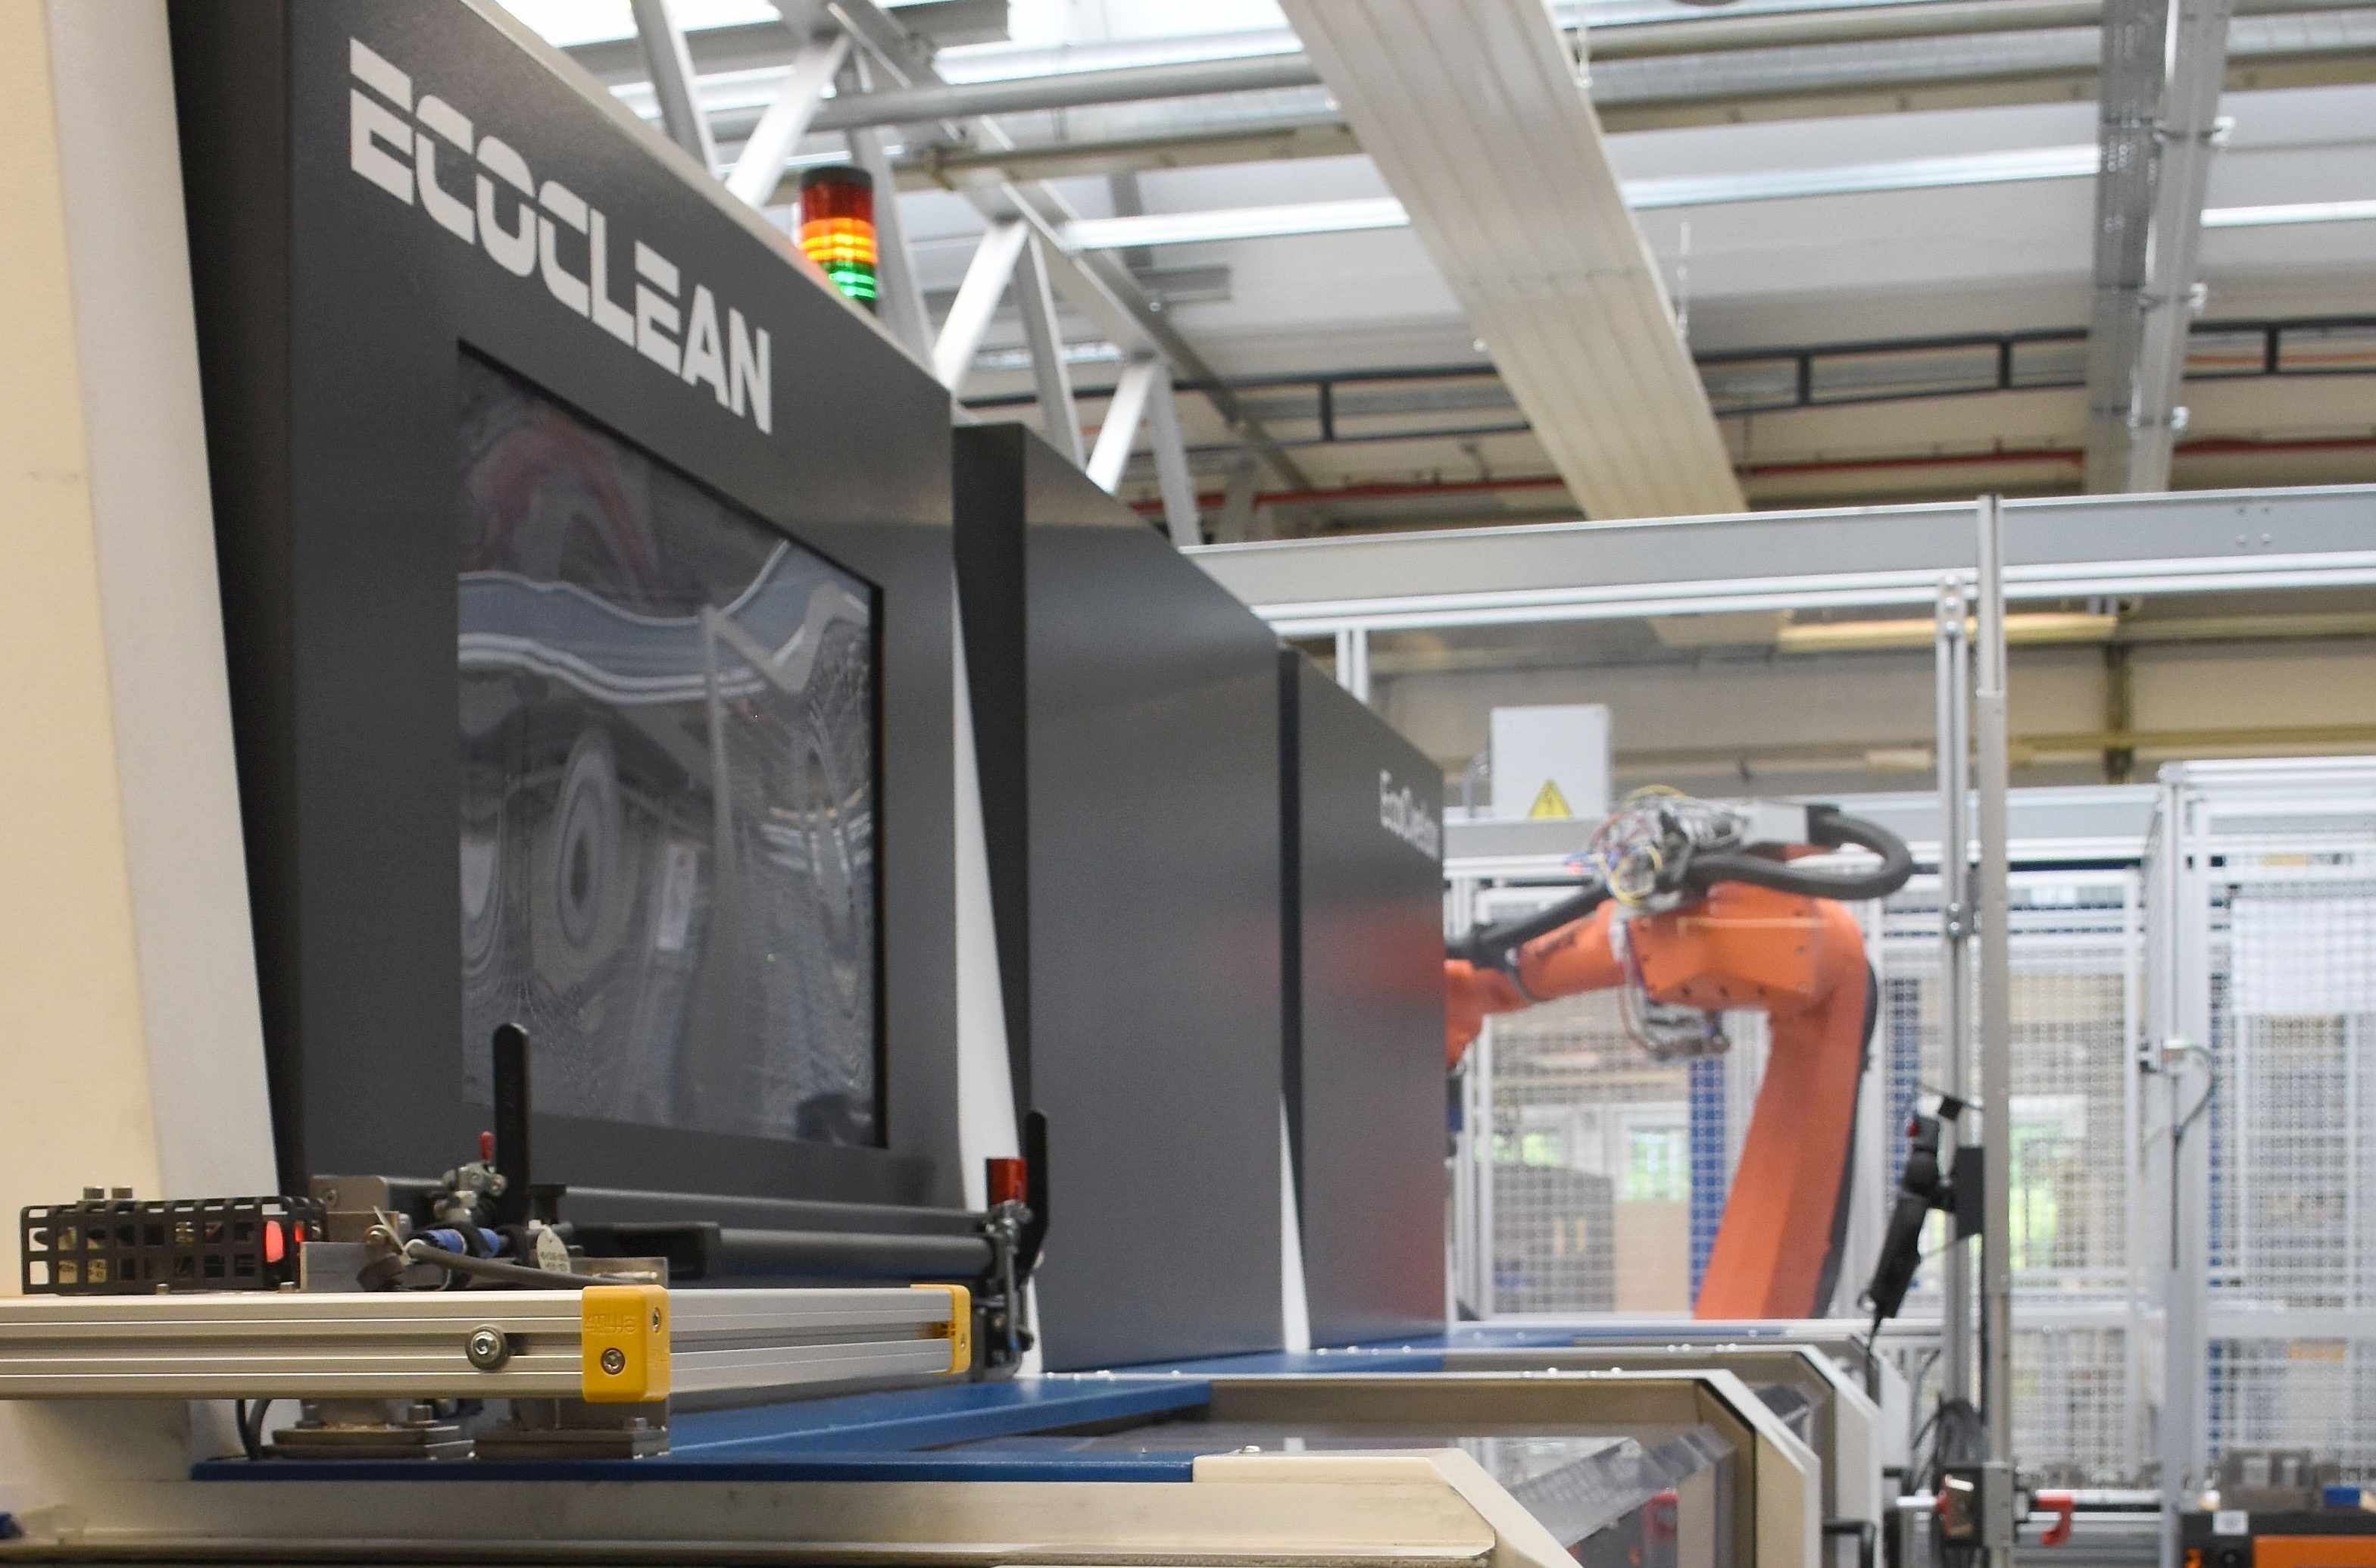
The decisive factor in the decision in favor of the EcoCvelox was, on the one hand, the design based on standard modules for targeted high-pressure deburring, cleaning and drying. This means that the system can be easily expanded if throughput requirements change. On the other hand, the wide range of components can be flexibly mapped by feeding the parts on different workpiece carriers.
The workpiece carriers are transported between the processing units by a standard integrated, highly dynamic linear system with a wear-free motor. "The alternative would have been a system in which robots grab the parts and move them past the various lances. To realize this in our short cycle times would have required a very large number of robots doing the same task. In addition, the humid atmosphere in a cleaning system causes increased maintenance work on the robots, which reduces system availability," adds Erik Müller. The EcoCvelox also scored points for its CAD/CAM interface, which is integrated as standard and can also be found on machine tools.
(Kopie 13)
Processes tailored to requirements
An Ecoclean system consisting of three modules - targeted high-pressure deburring, cleaning and drying - is integrated into the production line at Bosch Rexroth. Due to the short cycle times, the high-pressure unit has an optional second Y-axis for parts handling. Loading and unloading can thus be carried out in parallel with machining. The module is also equipped with a high-pressure turret designed for four tools, which is currently equipped with two tools adapted to the application. In the cleaning and drying unit, a second chamber each also contributes to very short cycle times through parallel loading and unloading.
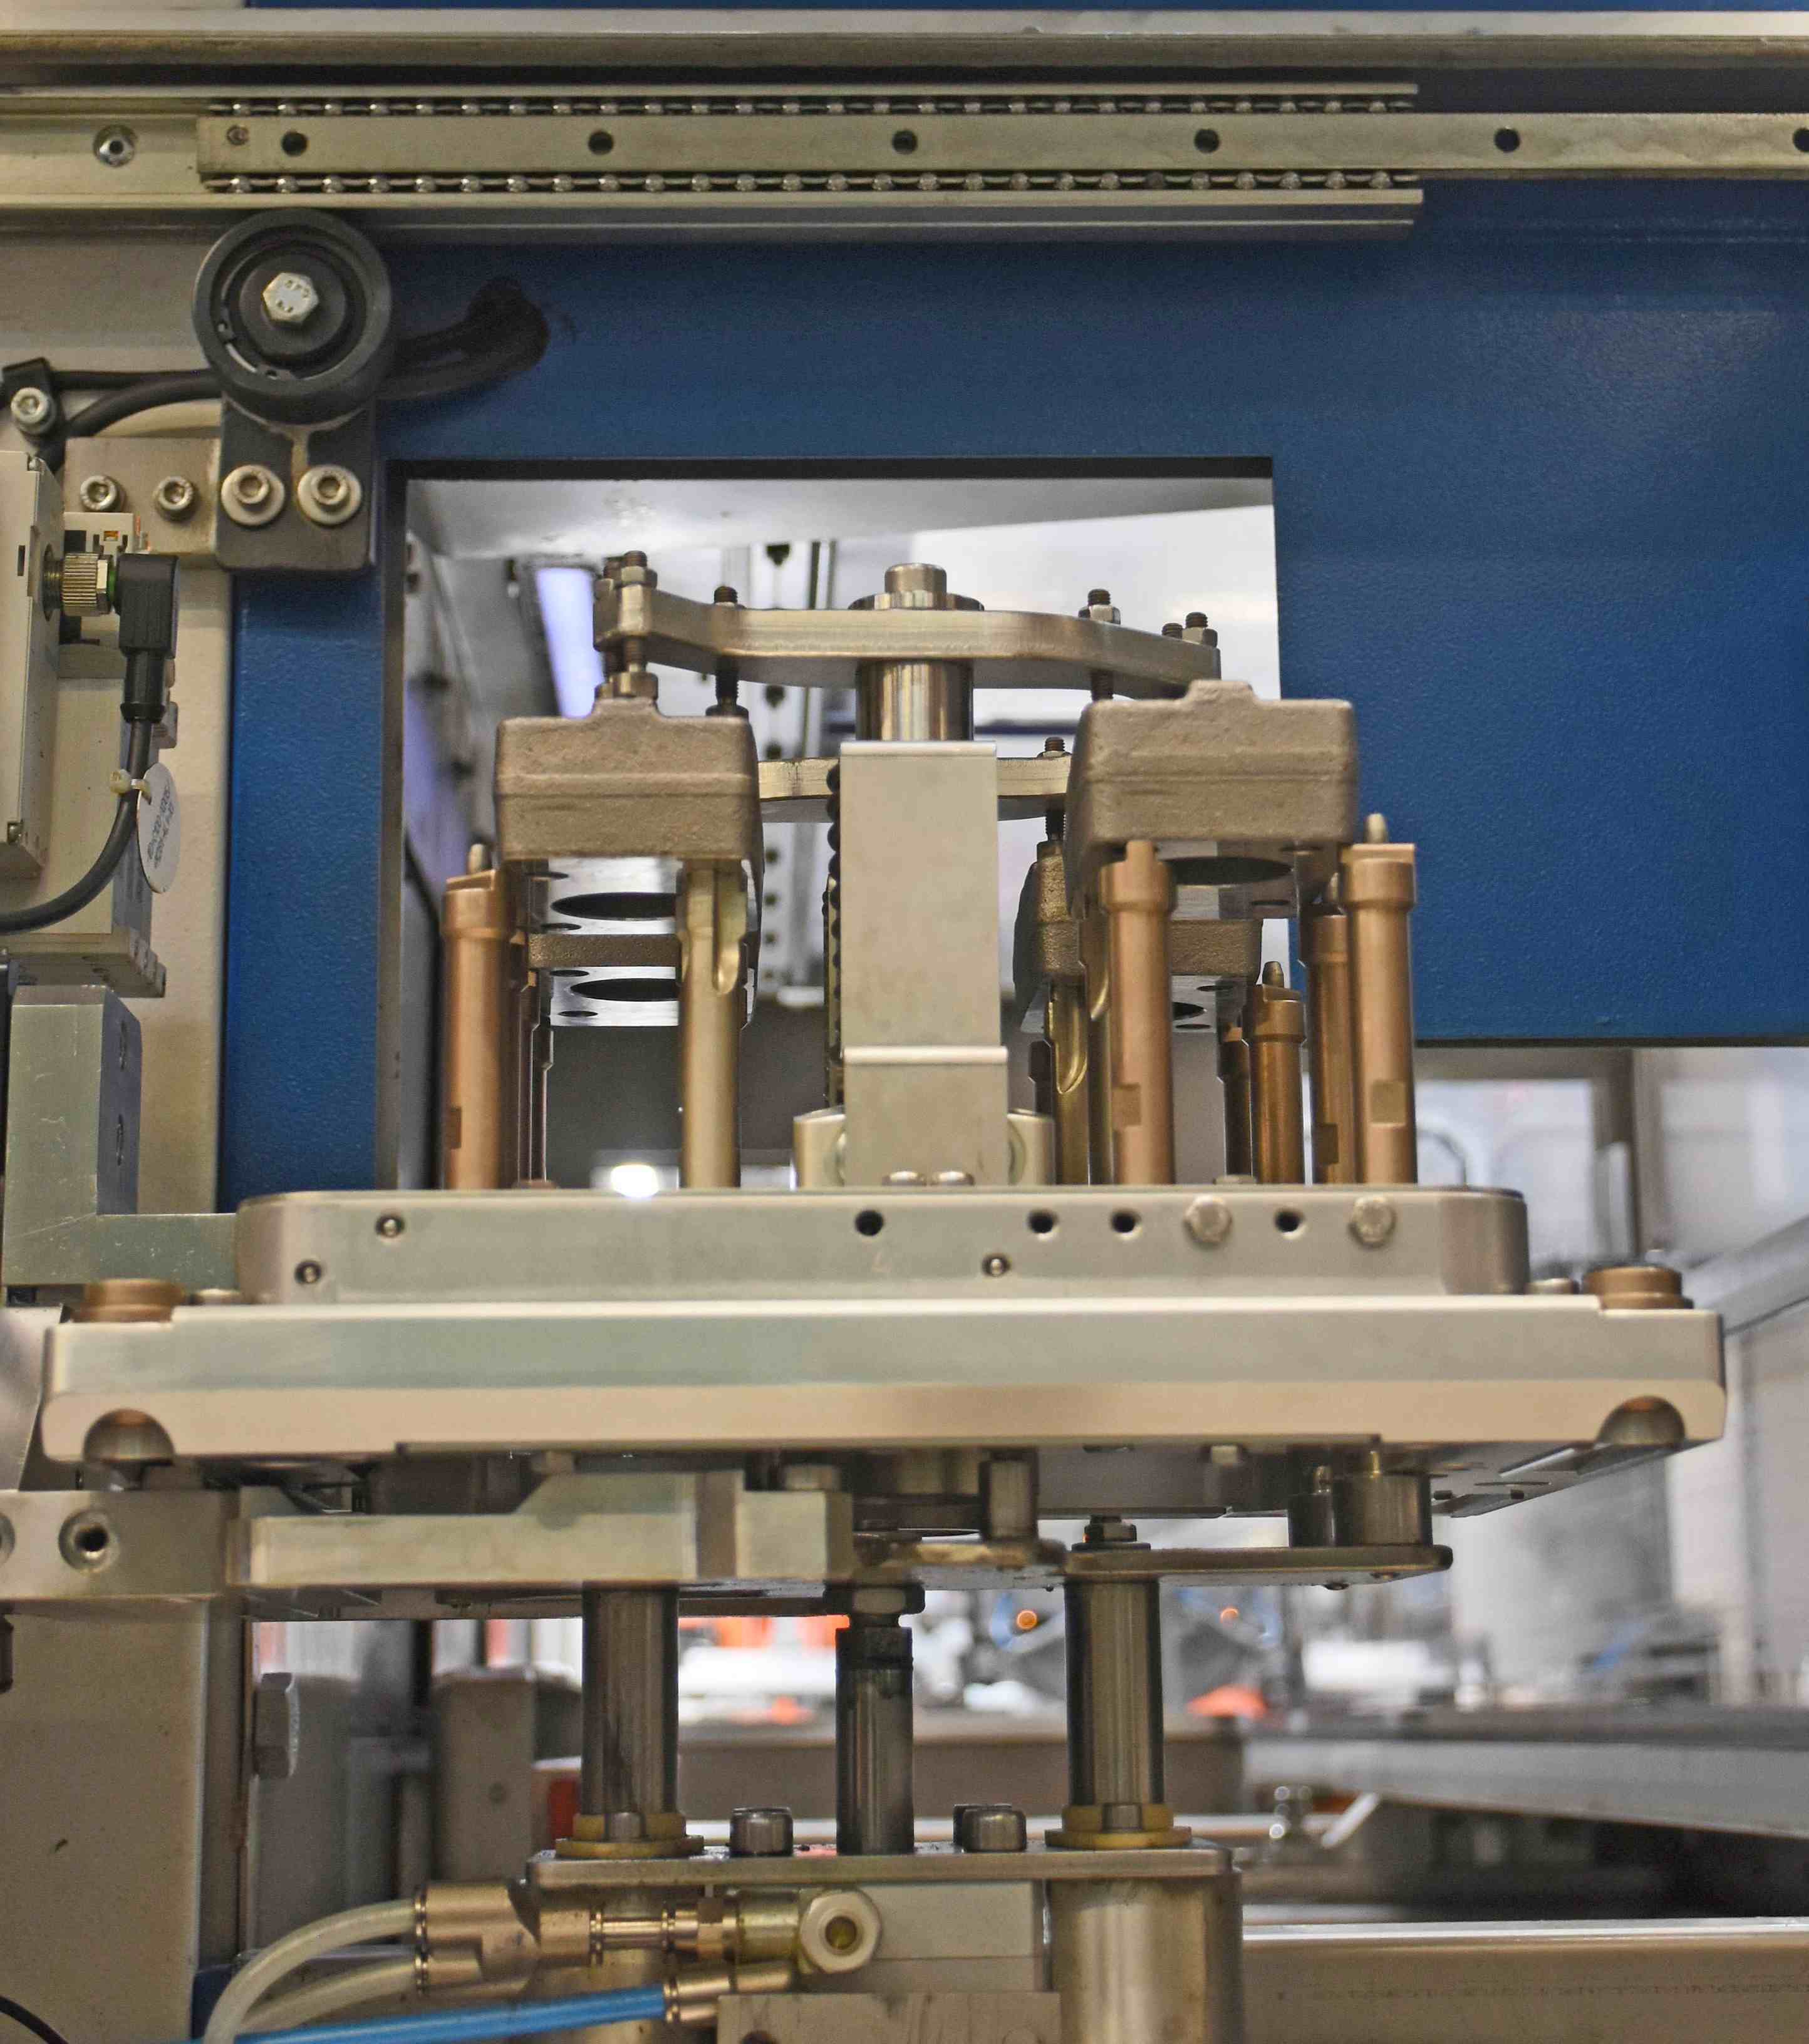
For cleaning, the parts made of forged steel and gray cast iron are clamped onto the workpiece carriers in series operation by means of robots. Manual loading is also possible. In total, only nine different workpiece carriers are used for the approximately 240 component variants. They are loaded with one to four parts depending on the workpieces to be cleaned.

One workpiece carrier - many parts
"It was a great feat of thinking to get as many parts as possible from different families onto one workpiece carrier. The design departments of Ecoclean and Bosch Rexroth worked very well together to achieve this," notes Eva Nowak. The cleaning process is preceded by a honing or deburring process. Since the latter also involves machining outer edges, the high-pressure deburring module is currently used primarily for targeted cleaning of the bores with the lances of the turret. This is done at a workpiece-specific pressure of up to 600 bar.
One workpiece carrier - many parts
"It was a great feat of thinking to get as many parts as possible from different families onto one workpiece carrier. The design departments of Ecoclean and Bosch Rexroth worked very well together to achieve this," notes Eva Nowak. The cleaning process is preceded by a honing or deburring process. Since the latter also involves machining outer edges, the high-pressure deburring module is currently used primarily for targeted cleaning of the bores with the lances of the turret. This is done at a workpiece-specific pressure of up to 600 bar.
"The removal of internal burrs with the EcoCvelox is a technological leap that we are currently reserving for ourselves. As soon as the new finishing line is fully interlinked and running smoothly, we will start process optimization, which includes deburring," reports Erik Müller. For component cleaning in the subsequent cleaning module, the processes injection flood washing, spray cleaning and targeted rinsing are available and can be combined. In the drying unit, a high-speed blow-off first takes place, followed by vacuum drying.
After cleaning, the parts pass through various cleanliness checks according to requirements. "The system must be cleared for the products of each component family. For this purpose, we carry out checks for particulate cleanliness in accordance with VDA 19 as well as for surface tension. Other essential criteria include paint adhesion strength and corrosion protection," notes Eva Nowak.
The CAD/CAM interface has proven to be a significant simplification, not only in optimizing the process parameters, but also in creating the 35 part-specific deburring/cleaning programs used to date. This is because it enables data from the component design to be transferred for programming, which is carried out offline. The program is then simply imported into the system control. This allows the cleaning/deburring of future product families and new components to be integrated just as effectively and economically as the machining of parts in batch size 1.
(Kopie 8)
Pilot customer for cleaning small batches in cycle
"Training for programming had to take place online due to the Corona pandemic. Ecoclean's staff did a good job, because today our colleagues say that programming is quick and easy to do and fun," adds Eva Nowak. "It is certainly not usual for a company like Bosch Rexroth to become a pilot customer for a completely newly developed system and thus leave proven paths. But the concept of this cleaning solution convinced us right from the start and also offers us reserves for future developments," Erik Müller notes in conclusion.
(Kopie 6)
Ecoclean GmbH
www.ecoclean-group.net
Bosch Rexroth AG
www.boschrexroth.com